 North American Safety Valve Industries, Inc.North American Safety Valve Industries, Inc.North American Safety Valve Industries, Inc.
Choosing a hydraulic relief valve in 2026 requires more than comparing catalog prices. The valve must protect the pump, actuator, piping, and people nearby. It also must respond predictably when pressure rises suddenly. Small errors can create heat, noise, leakage, or costly downtime.
Hydraulic systems author Anthony Esposito once wrote, “A relief valve is not merely a safety component; it is part of the system’s control strategy.” That principle remains practical today. Start with the maximum allowable system pressure, not the pump’s theoretical rating. Then check flow capacity, cracking pressure, adjustment range, fluid type, operating temperature, and contamination levels. A valve that looks suitable on paper may perform poorly beside a hot pump outlet or a long, narrow return line.
Measure the real conditions.
Field experience matters here. Record peak pressure during cold starts, cylinder stoppage, and rapid directional changes. Compare those readings with the valve’s pressure-flow curve. Review whether the valve is direct-acting or pilot-operated. Direct-acting models often suit compact, fast-response circuits. Pilot-operated designs may manage higher flows with less pressure loss. Neither choice is automatically better.
Do not ignore installation details. Incorrect port orientation, undersized piping, or unstable adjustment can defeat a high-quality hydraulic relief valve. Testing should follow the manufacturer’s instructions and applicable safety practices. I would also leave room for doubt: calculated flow may differ from field flow, especially after years of contamination and seal wear. A careful selection process accepts that uncertainty, verifies assumptions, and treats maintenance access as part of valve performance.
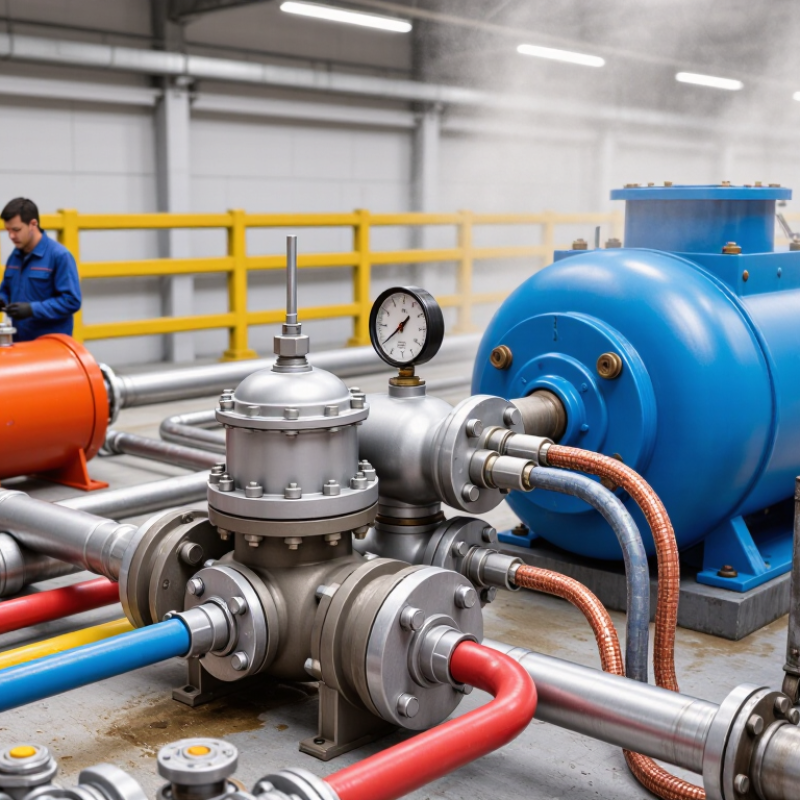
How to Choose a Hydraulic Relief Valve in 2026?
Pressure ratings need careful interpretation. A valve marked 210–420 bar does not mean every setting is safe. It describes an adjustable operating range or pressure class, depending on the manufacturer’s specification. ISO 4413:2010 requires hydraulic systems to include pressure-limiting protection and suitable component ratings. The relief setting must remain below the weakest rated component, not merely below the pump’s maximum pressure.
Start with the real system limit. A circuit operating at 350 bar may require a 420-bar-rated valve, but only after checking continuous pressure, pressure spikes, temperature, and flow capacity. A 210-bar valve is unsuitable, even if its threads fit. That mistake is surprisingly common. The valve must also discharge the pump’s full flow without creating damaging backpressure. Contamination control matters too; ISO 4413 links safe performance with cleanliness and proper maintenance.
Market data shows why selection deserves engineering review. Grand View Research estimated the global hydraulic equipment market at about USD 49.6 billion in 2023, reflecting extensive use in high-load machinery. However, market growth does not guarantee safe design. Field assessments often reveal relief valves set too close to maximum pressure, especially after pump replacements. That shortcut deserves reconsideration. Record the measured setting, verify the pressure gauge, and test the valve under realistic temperature and load conditions. A pressure spike may last milliseconds, yet still damage seals, hoses, or manifolds.
| Selection Dimension | 210 bar Class | 280 bar Class | 350 bar Class | 420 bar Class | ISO 4413-Oriented Check |
|---|---|---|---|---|---|
| Nominal pressure rating | 210 bar 21 MPa / 3,046 psi |
280 bar 28 MPa / 4,061 psi |
350 bar 35 MPa / 5,076 psi |
420 bar 42 MPa / 6,092 psi |
Use the valve rating at the actual fluid temperature and duty cycle; do not treat nominal rating as the permitted system operating pressure. |
| Maximum system working pressure | Must be established by the system designer. | Must be established by the system designer. | Must be established by the system designer. | Must be established by the system designer. | Set the operating limit below the lowest pressure rating of all connected components, considering pressure spikes and tolerances. |
| Relief-valve setting | Select only after calculating required actuator force and flow. | Select only after calculating required actuator force and flow. | Select only after calculating required actuator force and flow. | Select only after calculating required actuator force and flow. | The setting must protect the weakest rated component and remain compatible with the pump, actuator, piping, and control strategy. |
| Required relief capacity | Size from the maximum flow that can reach the protected section. | Size from the maximum flow that can reach the protected section. | Size from the maximum flow that can reach the protected section. | Size from the maximum flow that can reach the protected section. | Confirm rated flow, pressure override, response behavior, and heat generation at the actual relief flow—not only at nominal pump flow. |
| Pressure type to compare | Working pressure | Working pressure | Working pressure | Working pressure | Keep working, proof, burst, and peak transient pressures separate. A proof-test value is not a continuous operating limit. |
| Fluid compatibility | Verify fluid type and seal material. | Verify fluid type and seal material. | Verify fluid type and seal material. | Verify fluid type and seal material. | Check mineral oil, water-glycol, phosphate-ester, biodegradable, or other fluid compatibility, including temperature limits. |
| Temperature consideration | Use the valve's documented temperature range. | Use the valve's documented temperature range. | Use the valve's documented temperature range. | Use the valve's documented temperature range. | Account for viscosity changes, seal aging, thermal expansion, and reduced component ratings at elevated temperature. |
| Installation location | Protect the intended pressure zone. | Protect the intended pressure zone. | Protect the intended pressure zone. | Protect the intended pressure zone. | Install relief protection so no component can be isolated from the protective device unless an equivalent safe arrangement is provided. |
| Adjustment and tamper control | Lock or seal the approved setting. | Lock or seal the approved setting. | Lock or seal the approved setting. | Lock or seal the approved setting. | Prevent unauthorized adjustment and document the setting, test method, date, and responsible person. |
| Noise and heat control | Check continuous unloading duty. | Check continuous unloading duty. | Check continuous unloading duty. | Check continuous unloading duty. | Avoid using a relief valve as a permanent flow-control device unless the thermal load, noise, and energy loss are specifically designed for. |
| Verification before commissioning | Pressure-test and function-check. | Pressure-test and function-check. | Pressure-test and function-check. | Pressure-test and function-check. | Confirm correct installation, leak-free connections, pressure indication, safe discharge routing, and emergency isolation procedures. |
| Important design note: ISO 4413 provides general rules and safety requirements for hydraulic fluid-power systems; it does not assign one universal relief-valve setting or require a single 210–420 bar rating. The final selection must be validated against the complete circuit schematic, component ratings, pressure transients, fluid, temperature, flow, applicable legislation, and the adopted edition of the relevant standards. | |||||